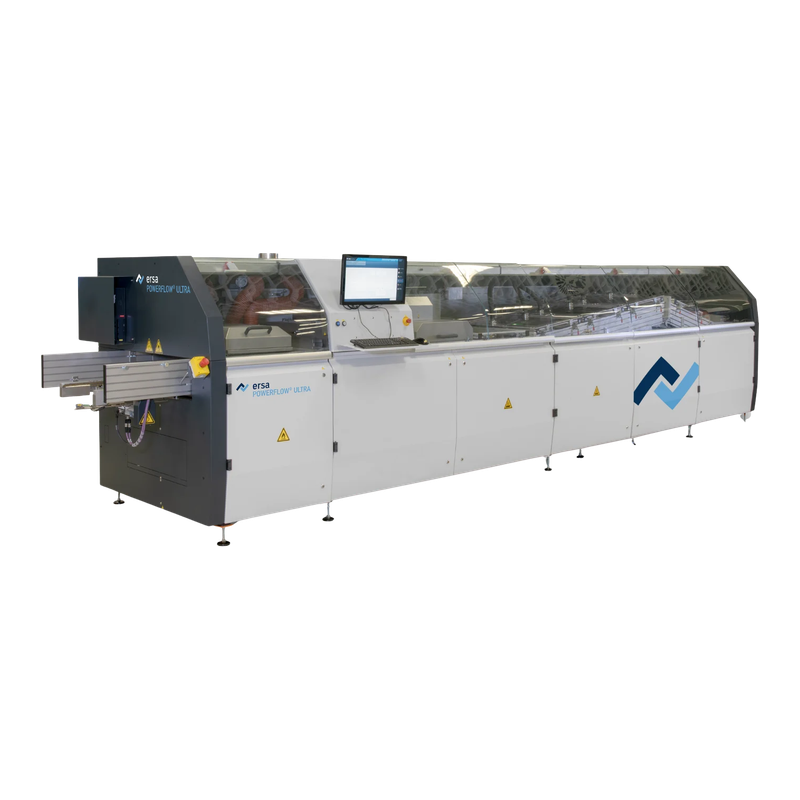
Base full-tunnel platform; reference illustration
POWERFLOW ULTRA
- Width
- Up to 406 mm finger transport
- Boundary
- Confirm frame transport and fitted preheat
SMT equipment sourcing · inspection · packing · global delivery
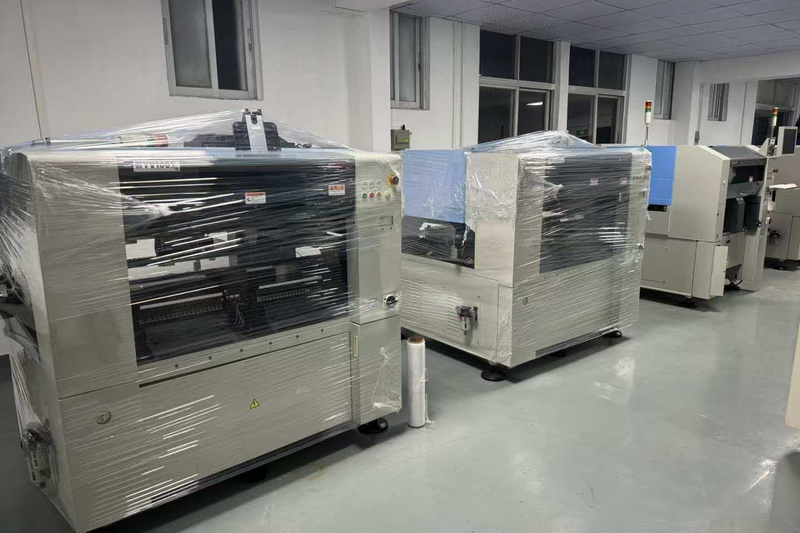
Ersa POWERFLOW ULTRA is a full-tunnel nitrogen wave soldering platform for through-hole and mixed assemblies. This family page keeps the base, XL and XXL working-width versions together and distinguishes them from POWERFLOW PRO, ONE and FIVE. The complete-machine reference illustration shows a labelled POWERFLOW ULTRA, not the fitted options or condition of a sale unit. Choose the required board, pallet, thermal mass and underside access before comparing ULTRA widths. A larger cabinet does not prove adequate flux coverage or acceptable hole fill. Do not transfer the newer POWERFLOW FIVE heavy-duty conveyor, wave-control or heating features to an ULTRA offer.
Apply flux to the required underside areas, preheat the supported assembly and pass its exposed joints over the configured solder waves in the nitrogen tunnel. Conveyor contact, wetting time, wave height, flux and thermal input must be qualified together; optional sequential soldering controls and tracing functions need installed evidence. Select by the actual board envelope, optical configuration and installation space—not the suffix alone.
Base full-tunnel platform; reference illustration
Wider working-envelope version
Largest working-envelope version
Manufacturer evidence checked 2026-10-07; numbers remain version-specific. Figures describe standard model configurations, not stock or an offered unit. Dimensions are listed in the source order and exclude the tower light where stated. The representative POWERFLOW ULTRA Family image is not proof of another version or an offered unit’s condition. Request nameplate, configuration and board-trial evidence before selection.
| Brochure finger-conveyor width | Base: 60–406 mm; XL: up to 520 mm; XXL: up to 610 mm |
|---|---|
| Board-length reference | Base/XL: 120–600 mm; XXL: up to 850 mm, subject to configuration |
| Conveyor and clearance | Finger or frame transport; 0.5–2.5 m/min; 80 mm top clearance, optionally up to 150 mm |
| Preheating configuration | 1.8 m standard reference; 2.4 or 3.0 m options using radiant and convection modules |
| Base cabinet reference | 5,700 × 1,400 × 1,580 mm; approximately 2,800 kg; transport/extensions change overall length |
| Lead-free solder volume | Base approximately 525 kg; XL 600 kg; XXL 700 kg in the brochure table; alloy and pot must match |
| Solder temperature | Maximum 300 °C catalogue limit, not a recommended setpoint for every alloy or assembly |
| Electrical reference | 5-wire 3 × 230/400 V, N, PE, 50/60 Hz; 3 × 125 A fuse reference; verify serial electrical drawings |
| Gas and extraction boundary | Nitrogen purity, flow, pressure and exhaust must match the serial installation; catalogue utility figures are not a site design |
The offer must identify POWERFLOW ULTRA version, serial, finger/frame conveyor, pallet capacity, fluxer, preheat modules, solder alloy/pot, nozzle combination, nitrogen and ERSASOFT release; Loaded-board thermal profile, flux coverage, hole fill and bridges, wave stability, transport and support, gas/extraction readings, cleaning access and authorized recipe recovery.
Ersa POWERFLOW ULTRA Family selection should begin with production requirements and evidence, not with a model name alone.
For a POWERFLOW ULTRA enquiry, send the complete PCB and pallet outline, loaded mass, component heights and underside features. The base, XL and XXL finger-conveyor limits are not the same as frame-transport dimensions. Ask for the actual fingers, adjustable rails, supports and permitted pallet mass to be identified and demonstrated. The photographed base platform does not establish a 610 mm XXL working width. Include edge clearance and fixture access to the joints when selecting a version rather than treating the largest catalogue board dimension as a universal production capability.
A good through-hole result depends on flux delivery, thermal input, contact time and board support together. Require the supplier to run the intended flux and solder alloy on a representative assembly, retain a populated-board temperature trace and inspect hole fill, bridging and heat-sensitive parts. Record the nozzle arrangement, conveyor angle and speed, wave height and settings used. Modular radiant and convection preheaters must be identified individually. A three-metre preheat option or the maximum 300 °C pot limit is not a process recipe, and an empty-conveyor demonstration cannot establish accepted-board throughput.
Retain the ULTRA nameplate, electrical drawings, solder-pot identity and authorized ERSASOFT software records. Catalogue solder capacity changes with base, XL, XXL and alloy; mixing a lead-free value with the SnPb-equivalent table creates an incorrect utility and handling estimate. Check the installed nozzle combination and whether sector-based sequential soldering, tracing or data interfaces are actually present and licensed. Do not borrow POWERFLOW FIVE Smart Wave Guard, heavy-duty conveyor or heating claims for an older ULTRA. Demonstrate recipe export and approved recovery as part of the offered configuration.
The nitrogen tunnel requires a reviewed site supply and extraction plan. Ask the responsible equipment team to reconcile pressure, purity, flow, exhaust and electrical requirements with the serial manual; differing legacy gas references must not be silently combined. Inspect safe maintenance access, flux deposits, transport lubrication and the cleaning path with the machine isolated. Manufacturer Ersa China and the independent Thinkfon import catalogue provide two exact ULTRA enquiry channels, not confirmed inventory. Neither was contacted. Require dated complete-machine views, the nameplate, location and a witnessed acceptance sequence before relying on a price or delivery promise.
Ersa POWERFLOW ULTRA Family should be evaluated against the buyer’s apply flux to the required underside areas, preheat the supported assembly and pass its exposed joints over the configured solder waves in the nitrogen tunnel. conveyor contact, wetting time, wave height, flux and thermal input must be qualified together; optional sequential soldering controls and tracing functions need installed evidence. The final application fit depends on the evidence for the specific unit.
These questions keep the quotation scope connected to the buyer’s real SMT process.
Ersa POWERFLOW ULTRA Family buyers should confirm this with actual-machine evidence before quotation.
Ersa POWERFLOW ULTRA Family buyers should confirm this with actual-machine evidence before quotation.
Ersa POWERFLOW ULTRA Family buyers should confirm this with actual-machine evidence before quotation.
Before shipment, review the relevant power-on, movement, operating state and visible condition for the specific offered unit.
Request a dated operating sequence of the offered Ersa POWERFLOW ULTRA Family. The model-image control requests evidence, not playback of a recorded video.
Request a unit-specific Ersa POWERFLOW ULTRA Family list for serial-correct conveyor fingers or pallets, fluxer consumables, nozzle and pump service items, seals, gas references and authorized controls documentation. Availability is not claimed on this review page.
Provide target assembly, process requirements, brochure finger-conveyor width, installed configuration and destination, required accessories and desired inspection evidence for the proposed Ersa POWERFLOW ULTRA Family.
Common questions for overseas buyers evaluating a Ersa POWERFLOW ULTRA Family.
Apply flux to the required underside areas, preheat the supported assembly and pass its exposed joints over the configured solder waves in the nitrogen tunnel. Conveyor contact, wetting time, wave height, flux and thermal input must be qualified together; optional sequential soldering controls and tracing functions need installed evidence. Choose the required board, pallet, thermal mass and underside access before comparing ULTRA widths. A larger cabinet does not prove adequate flux coverage or acceptable hole fill. Do not transfer the newer POWERFLOW FIVE heavy-duty conveyor, wave-control or heating features to an ULTRA offer.
POWERFLOW ULTRA version, serial, finger/frame conveyor, pallet capacity, fluxer, preheat modules, solder alloy/pot, nozzle combination, nitrogen and ERSASOFT release. Request the exact nameplate and option list.
The Ersa POWERFLOW ULTRA Family illustration is model-reference imagery, not a dated stock photograph. Serial, location, condition, price and running evidence require separate confirmation.
The V3 scrolling proof gallery is retained. It describes LCSMT export preparation, not the condition of a particular Ersa POWERFLOW ULTRA Family unit.
Share target assembly, process requirements, brochure finger-conveyor width, installed configuration and destination and inspection expectations. LCSMT can review whether an actual Ersa POWERFLOW ULTRA Family configuration is a practical match.