Buyer decision 1
Make the assembly the test object
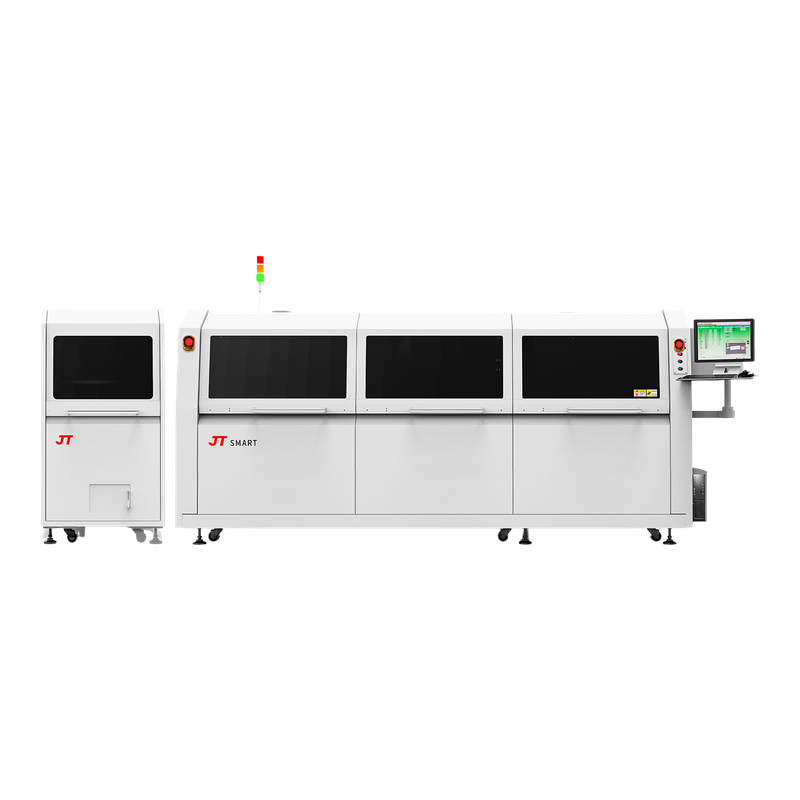
A wave-soldering machine should be selected for a defined assembly and process, not simply for a clean enclosure or the length of its heating section. JT SMART is described as a conveyor wave-soldering range with separated spray fluxing and a fixed transport angle. Those architecture facts help prepare a trial, but they do not establish a particular used machine’s state. Supply a populated sample, controlled drawing, solder alloy, flux and the process owner’s inspection criteria before the demonstration.
Buyer decision 2
Check support before applying heat
Record board thickness, loaded mass, component clearance, pallet outline and edge-support requirements. Observe transfer through loading, spray, preheat, soldering and unloading with the intended support arrangement. Look for sag, rubbing, a trapped pallet or inconsistent handoff. A successful empty conveyor test is not an acceptance result for the board. Since the published SMART transport angle is fixed, ask how the intended pallet and assembly are accommodated instead of assuming that angle can be adjusted.
Buyer decision 3
Connect spray coverage to the thermal record
Review flux compatibility with the process owner and document its delivery settings. Where a pallet is used, show access to the joints that need flux rather than observing only the spray nozzle. Measure the board’s thermal history at representative heavy and sensitive locations using an approved method. Keep the sample identity, sensor locations and settings. Do not infer acceptable soldering from a heater setpoint: board loading and preparation can differ even when the machine display is unchanged.
Buyer decision 4
Inspect more than the best-looking sample
Agree joint criteria using the board drawing and the buyer’s quality plan. Keep results from initial boards, repeated operation and a controlled stop/restart. Record adjustments, rejected boards and operator intervention. Investigate defects as a combination of incoming assembly, flux, heating, wave access and machine behavior; do not declare every defect a machine fault from one photograph. Likewise, do not discard failed samples and present one good board as a repeatability study.
Buyer decision 5
Request maintenance evidence safely
Ask for dated views of the actual nameplate, conveyor fingers, pot, nozzle, pump and flux area with the machine isolated according to the supplier’s safe procedure. Review deposits, corrosion, cleaning and relevant service records. During a supervised run, observe wave stability and board transfer. Fresh paint is not proof of mechanical condition. Any safety, electrical or exhaust assessment must be performed by qualified people; this checklist is a buying framework, not a substitute for their inspection.
Buyer decision 6
Decide what the trial establishes
The record should connect one machine serial, one installed configuration and one defined board/process to measured traces and inspection results. Common shortcuts are to judge the conveyor alone, equate preheat setpoints with board temperature, or accept a reference clip as unit evidence. A first-board result does not guarantee other pallets or assemblies. If only selected joints need soldering, compare a selective system such as NIS instead of assuming that a full-width wave is the correct process for every board.
Technical Sources
Manufacturer context and limits
Checked 4 October 2026. Published model facts support the examples; the acceptance framework is buyer guidance, not claimed LCSMT field-test evidence.