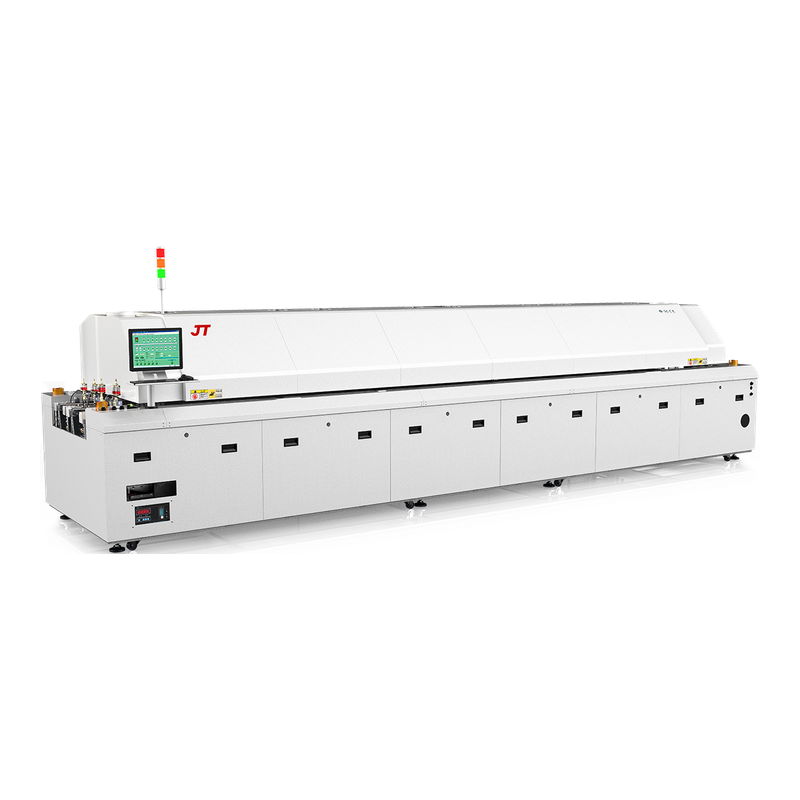
Air or Nitrogen Reflow: What Evidence Justifies the Choice?
Separate the assembly’s process requirement from the oven’s gas-system claim. Compare loaded-board profiles, oxygen measurements and operating obligations before choosing air or nitrogen.
SMT equipment sourcing · inspection · packing · global delivery
SMT Classroom
Explore SMT processes, inspection methods and practical buying guidance. Start with a question. Learn what to check next.
44 practical guides · 5 learning topics

44 guides · Showing 31–40 · Page 4 of 5

Separate the assembly’s process requirement from the oven’s gas-system claim. Compare loaded-board profiles, oxygen measurements and operating obligations before choosing air or nitrogen.

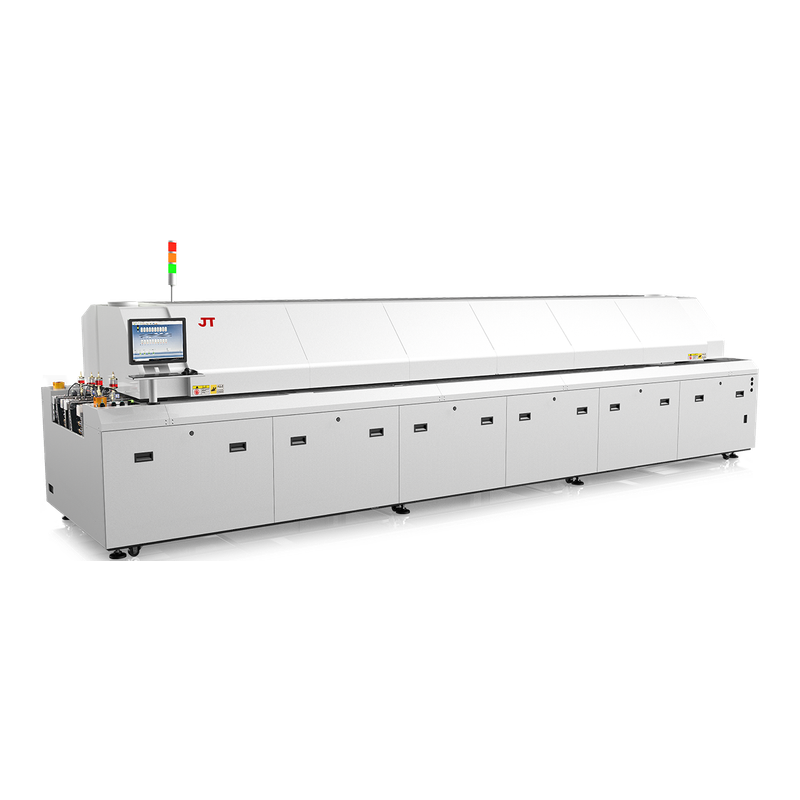
A clean exterior and a low exit-temperature claim do not reveal the installed cooling or residue-management system. Turn both into a documented inspection and acceptance scope.

A computer that starts is not a recoverable production system. Check controller identity, recipe restoration, licenses and safe restart ownership before accepting a used reflow oven.

Camera, sampling, board handling and cycle time are related configuration choices. Keep the columns separate and qualify paste measurements on the actual offered SPI generation.

A minimum pixel size and a maximum component height may describe different operating modes. Qualify hidden-joint images, board handling and review work together before buying inline AXI.

Two conveyor lanes do not prove twice the useful inspection capacity. Test board envelopes, identity, exceptions and review workload as one configuration.

A vacuum setting or attractive X-ray image is not a production result. Link the thermal profile, evacuation sequence and joint measurement before accepting a void-reduction claim.

Core cycle, complete print cycle and sustained good-board output are different measures. Include the cleaning schedule and paste results when comparing printer offers.

A running placement head does not establish a usable feeder investment. Match feeder generations, head options, program identity and first-board evidence before accepting a used mounter.

A conveyor can exchange ready signals yet still catch a board at the handoff. Build the acceptance check around rail alignment, support, clearance and a repeatable transfer.